
 3851
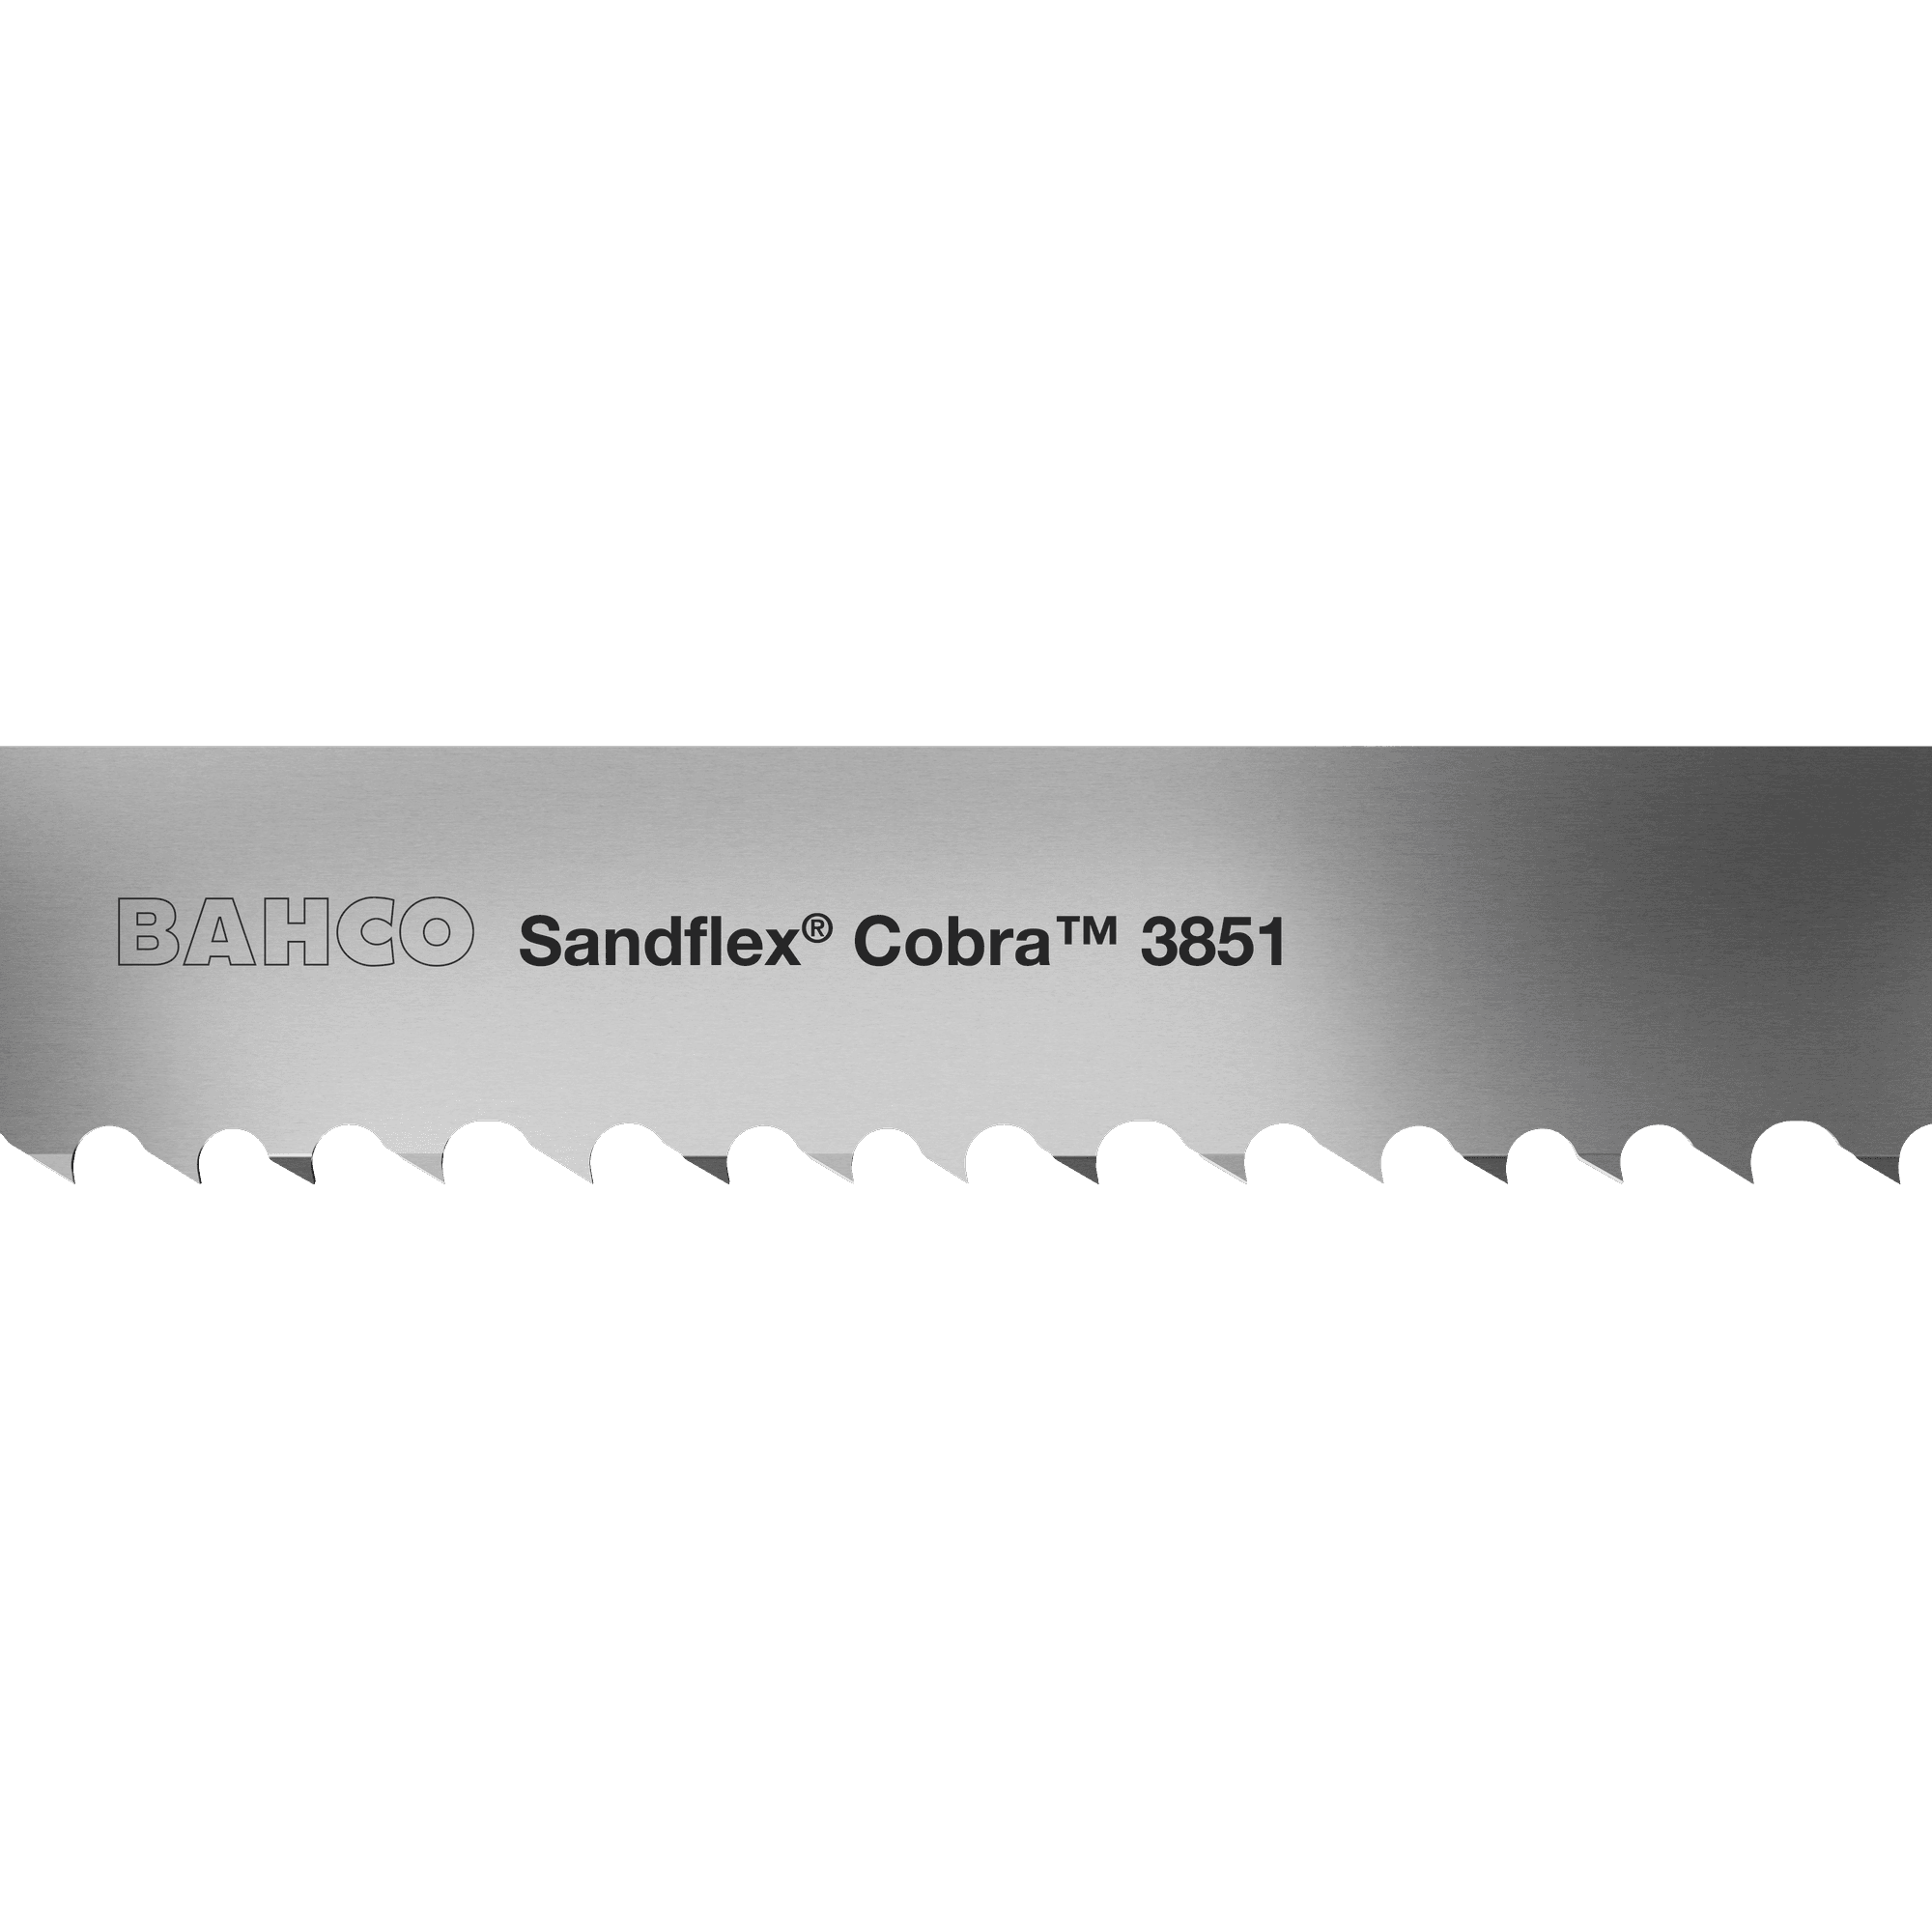
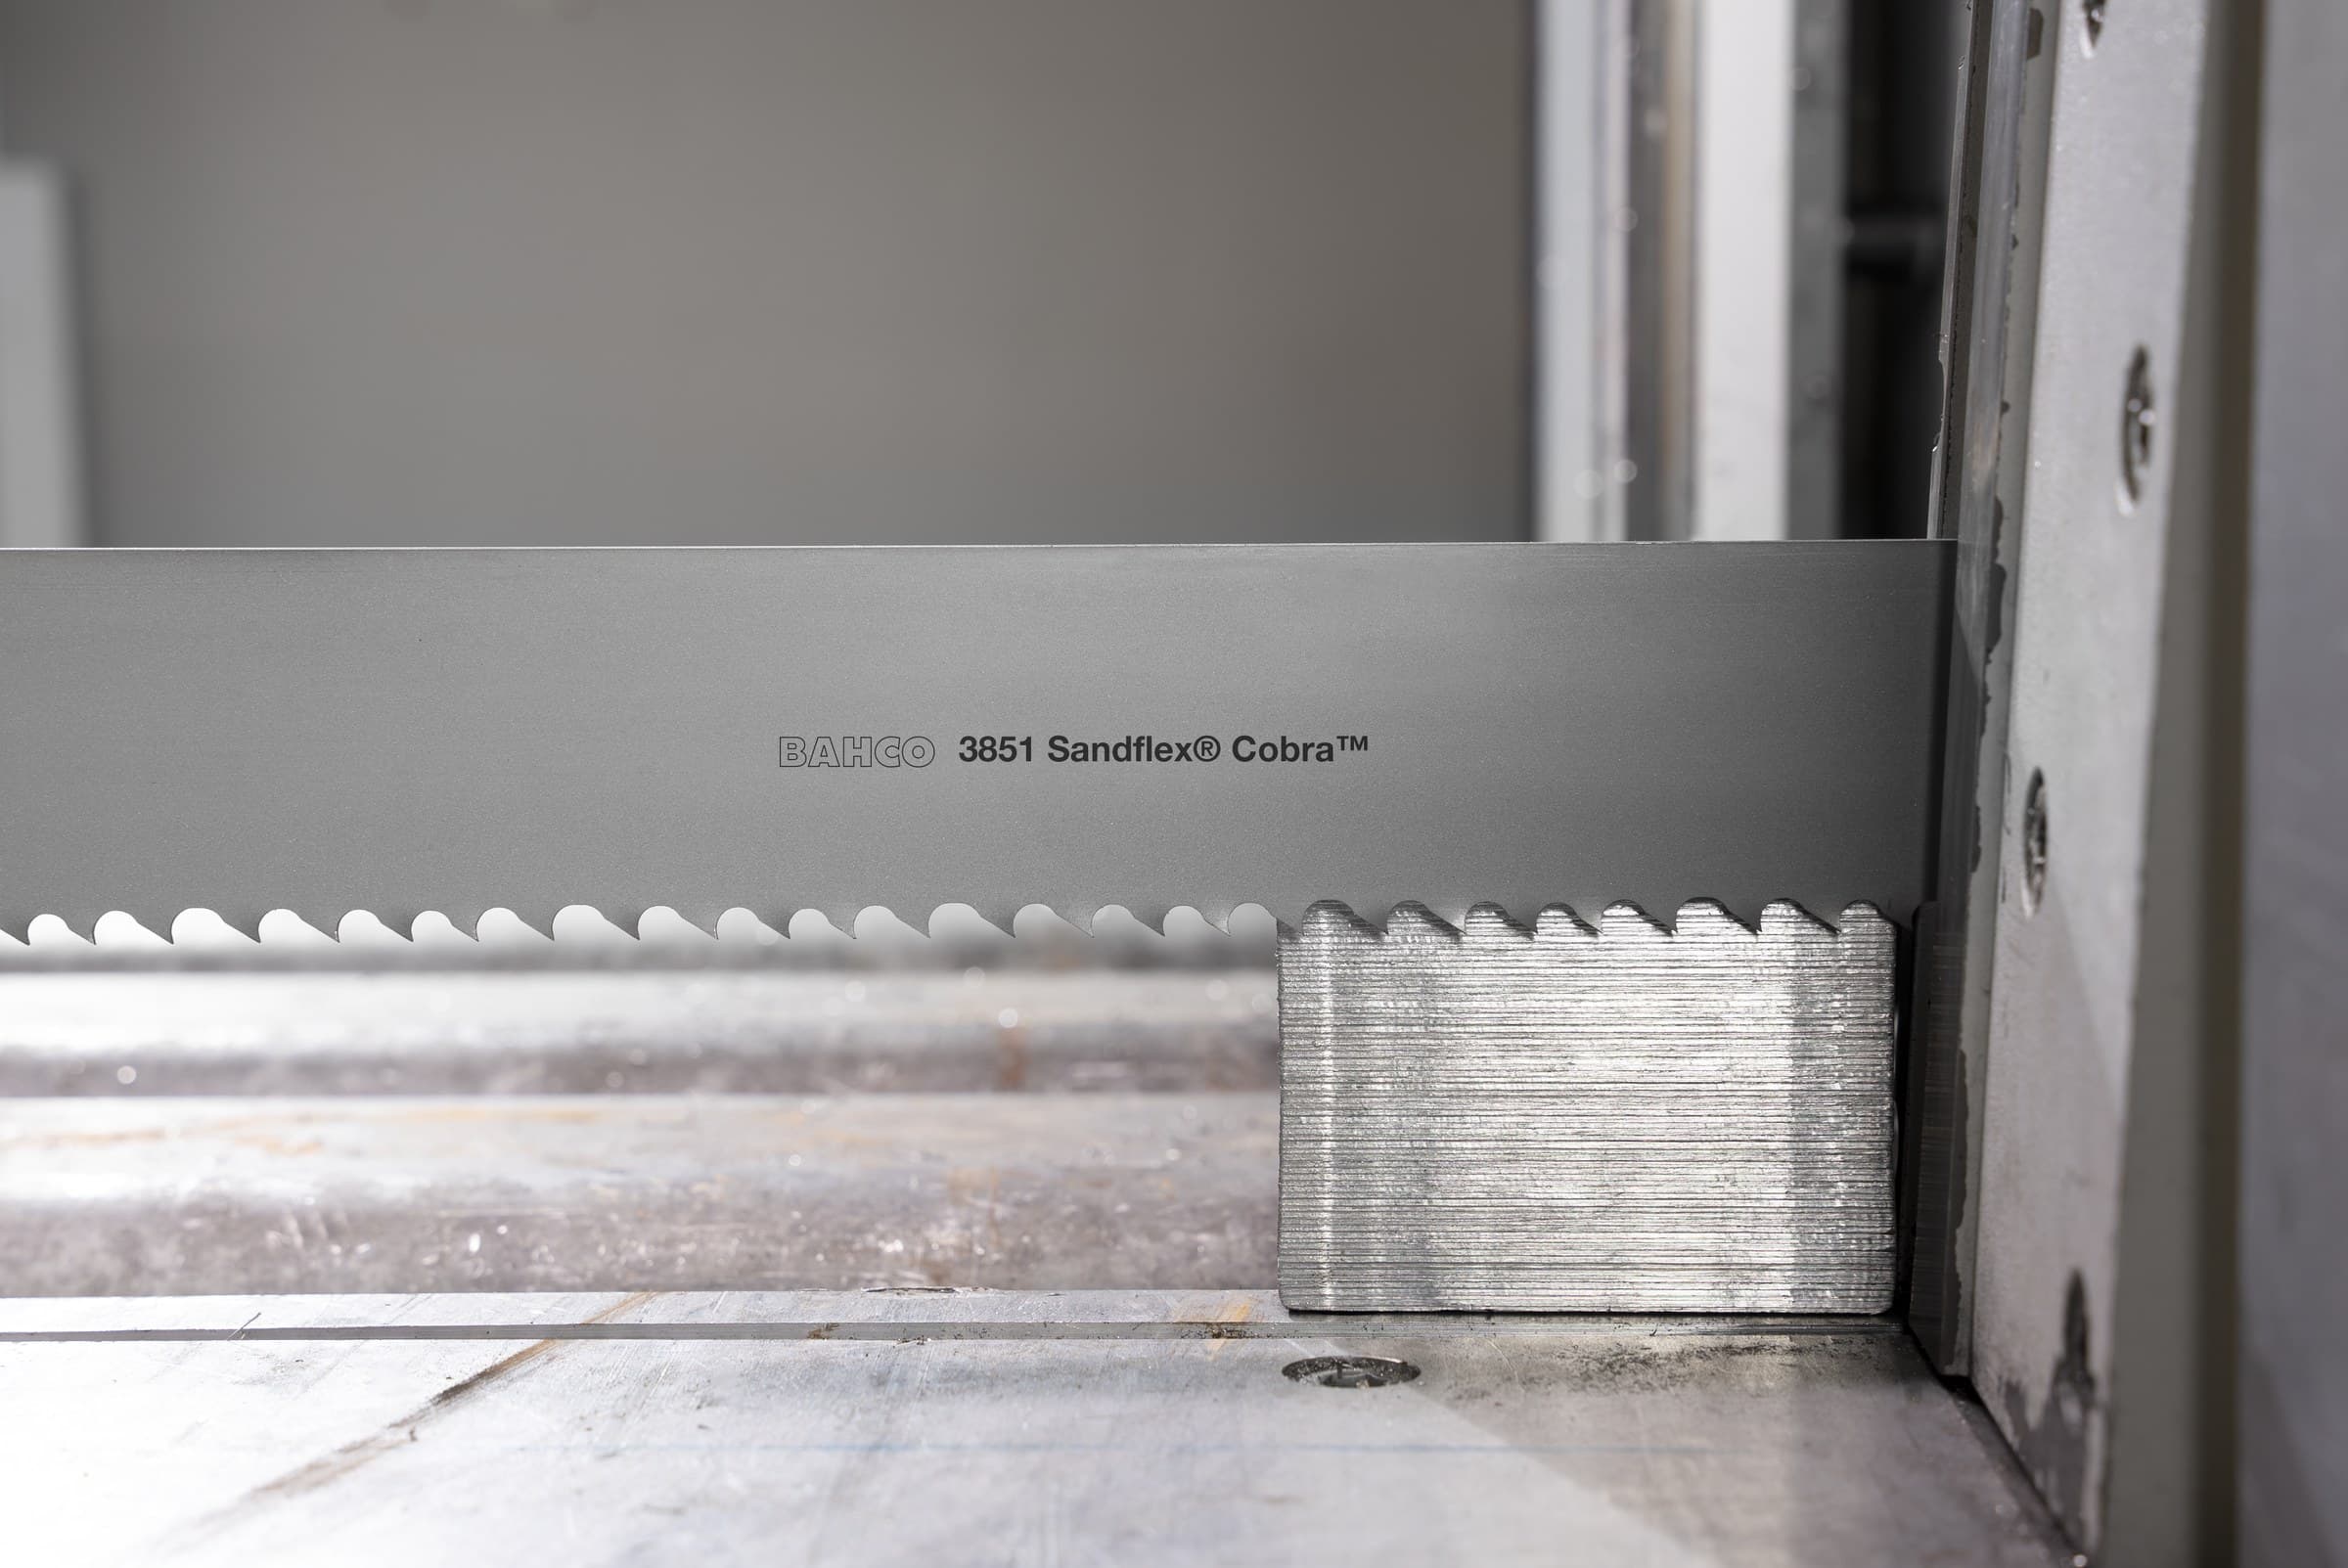
3851 Sandflex Cobra PRX Bandsaw Blade
Production bi-metal blade with an improved HSS tooth edge for high performance metal cutting.
Made to order and welded to the length you enter.
This blade
The size you have chosen above, with the range's published details.
27 x 0.9mm, 2/3 TPI, PRX
| Width | 27mm |
|---|---|
| Thickness | 0.9mm |
| TPI | 2/3 (variable pitch) |
| Tooth form | PRX |
| Pricing | By length: the band plus the weld |
| Lengths | Welded from 1,000mm to 8,000mm |
| Brand | Bahco |
| Product code | 3851 |
| Construction | HSS tooth edge welded to a flexible alloy steel backing |
| Cuts | Steel, Stainless steel |
| Edge and tooth notes | Improved HSS tooth edge |
| Verification source | Manufacturer product page |
Tooth form
What the manufacturer publishes about the tooth form of this blade.
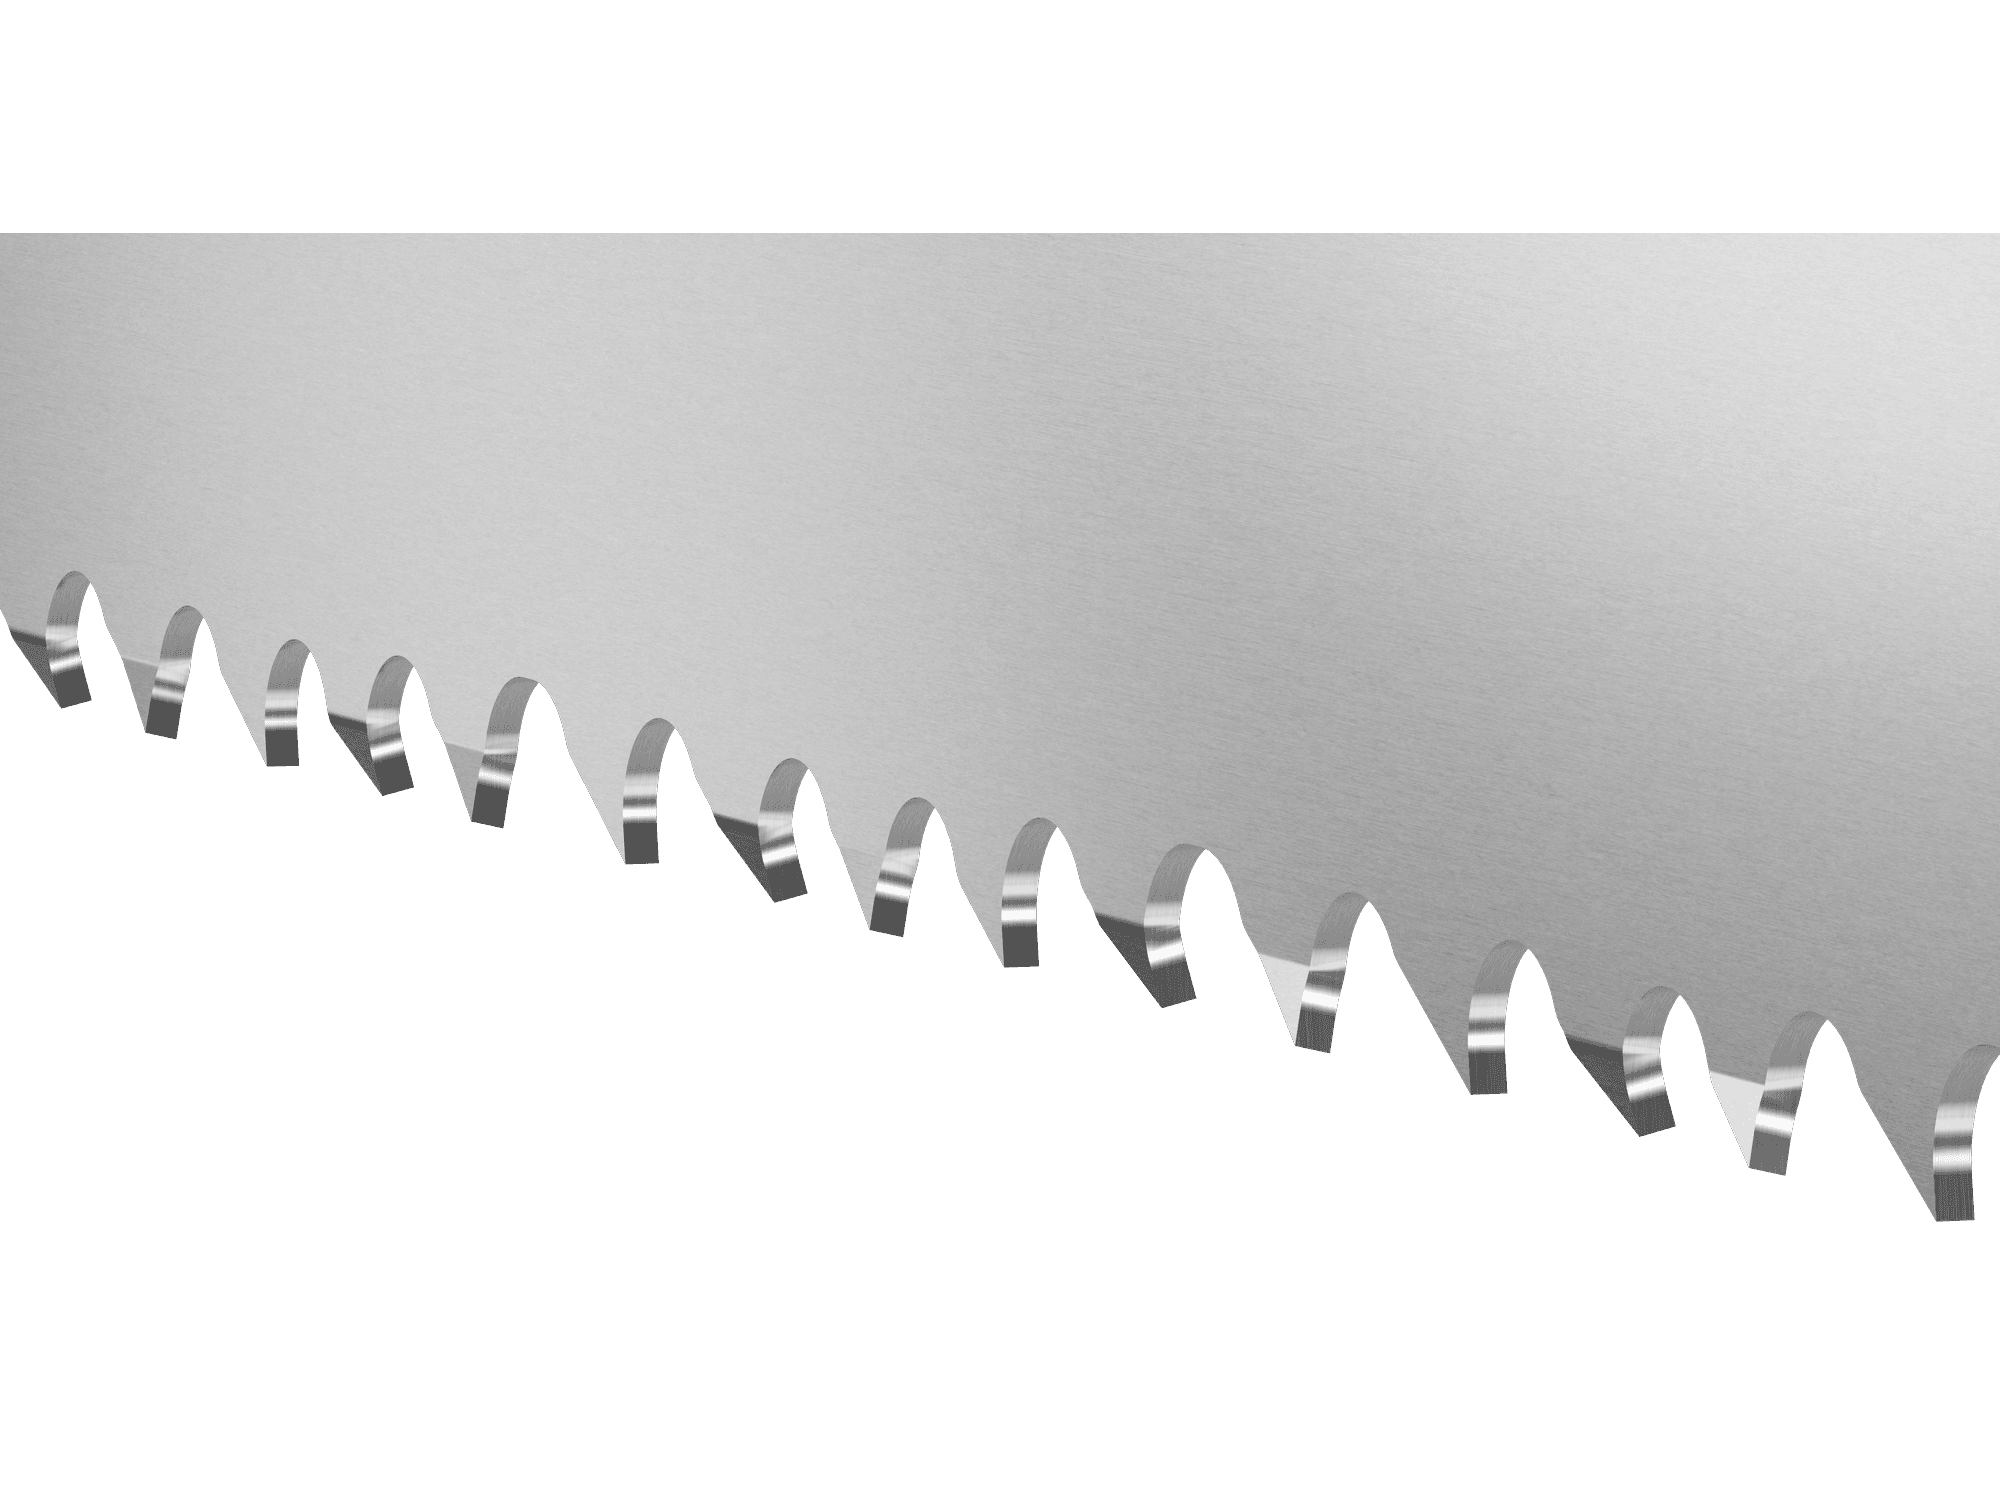
- PRX tooth
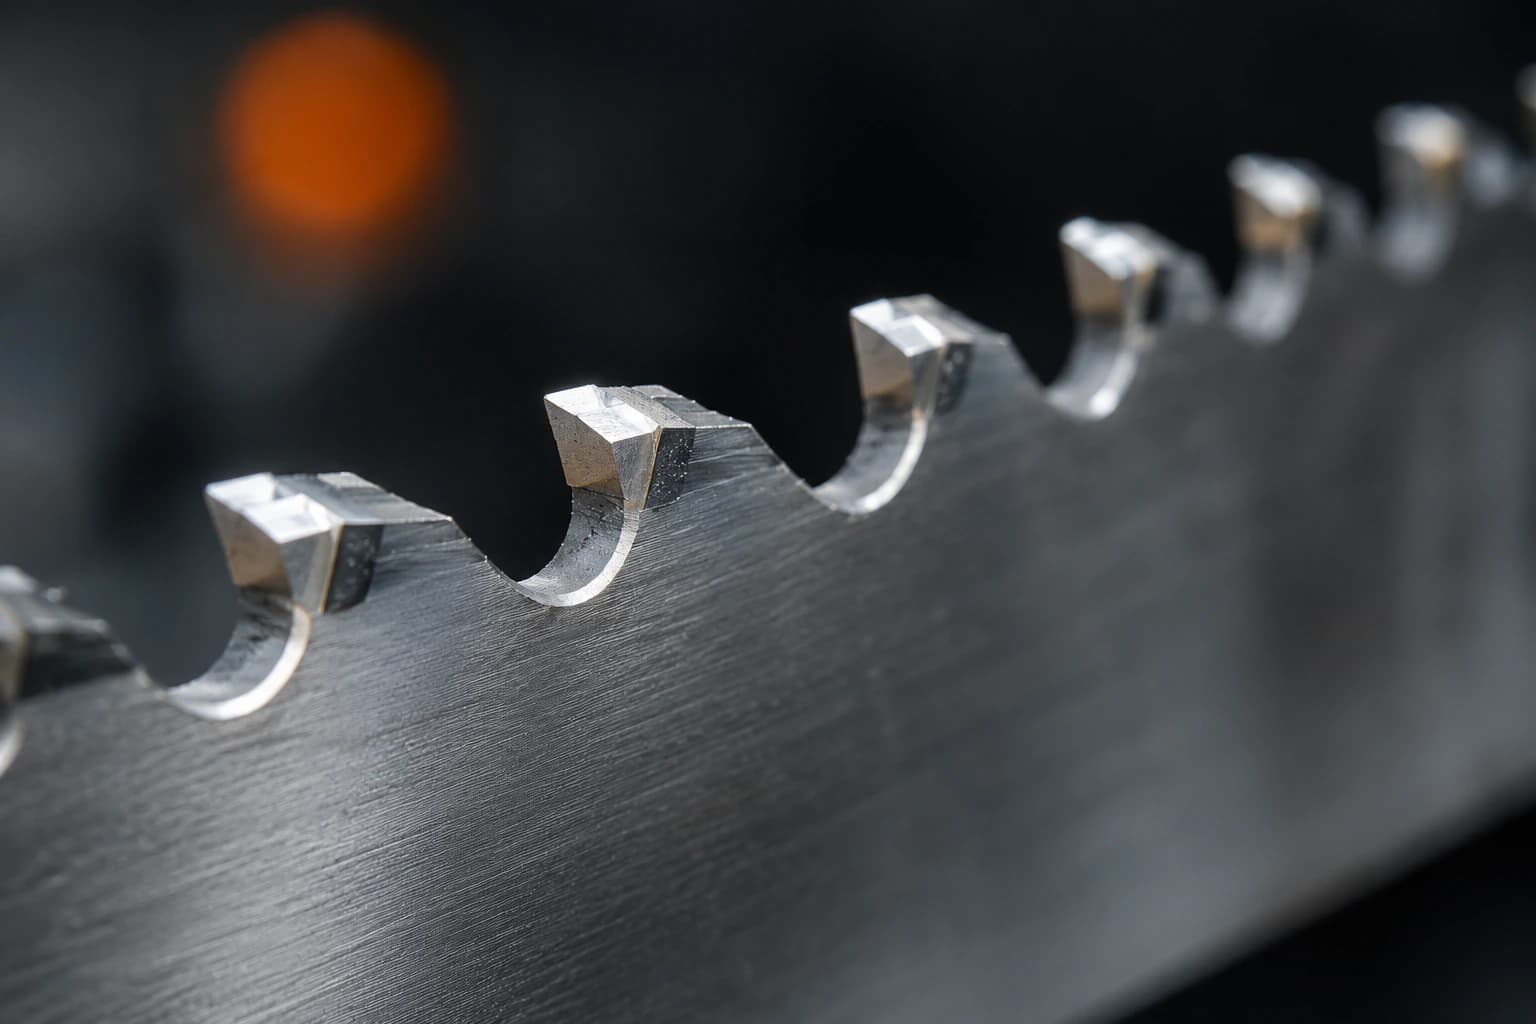
- Bahco presents PRX as its general purpose tooth for contour cutting and smaller machines, on an M42 high speed steel edge. Bahco does not publish a rake angle for it.
- Source: Bahco's published range.
Set and kerf
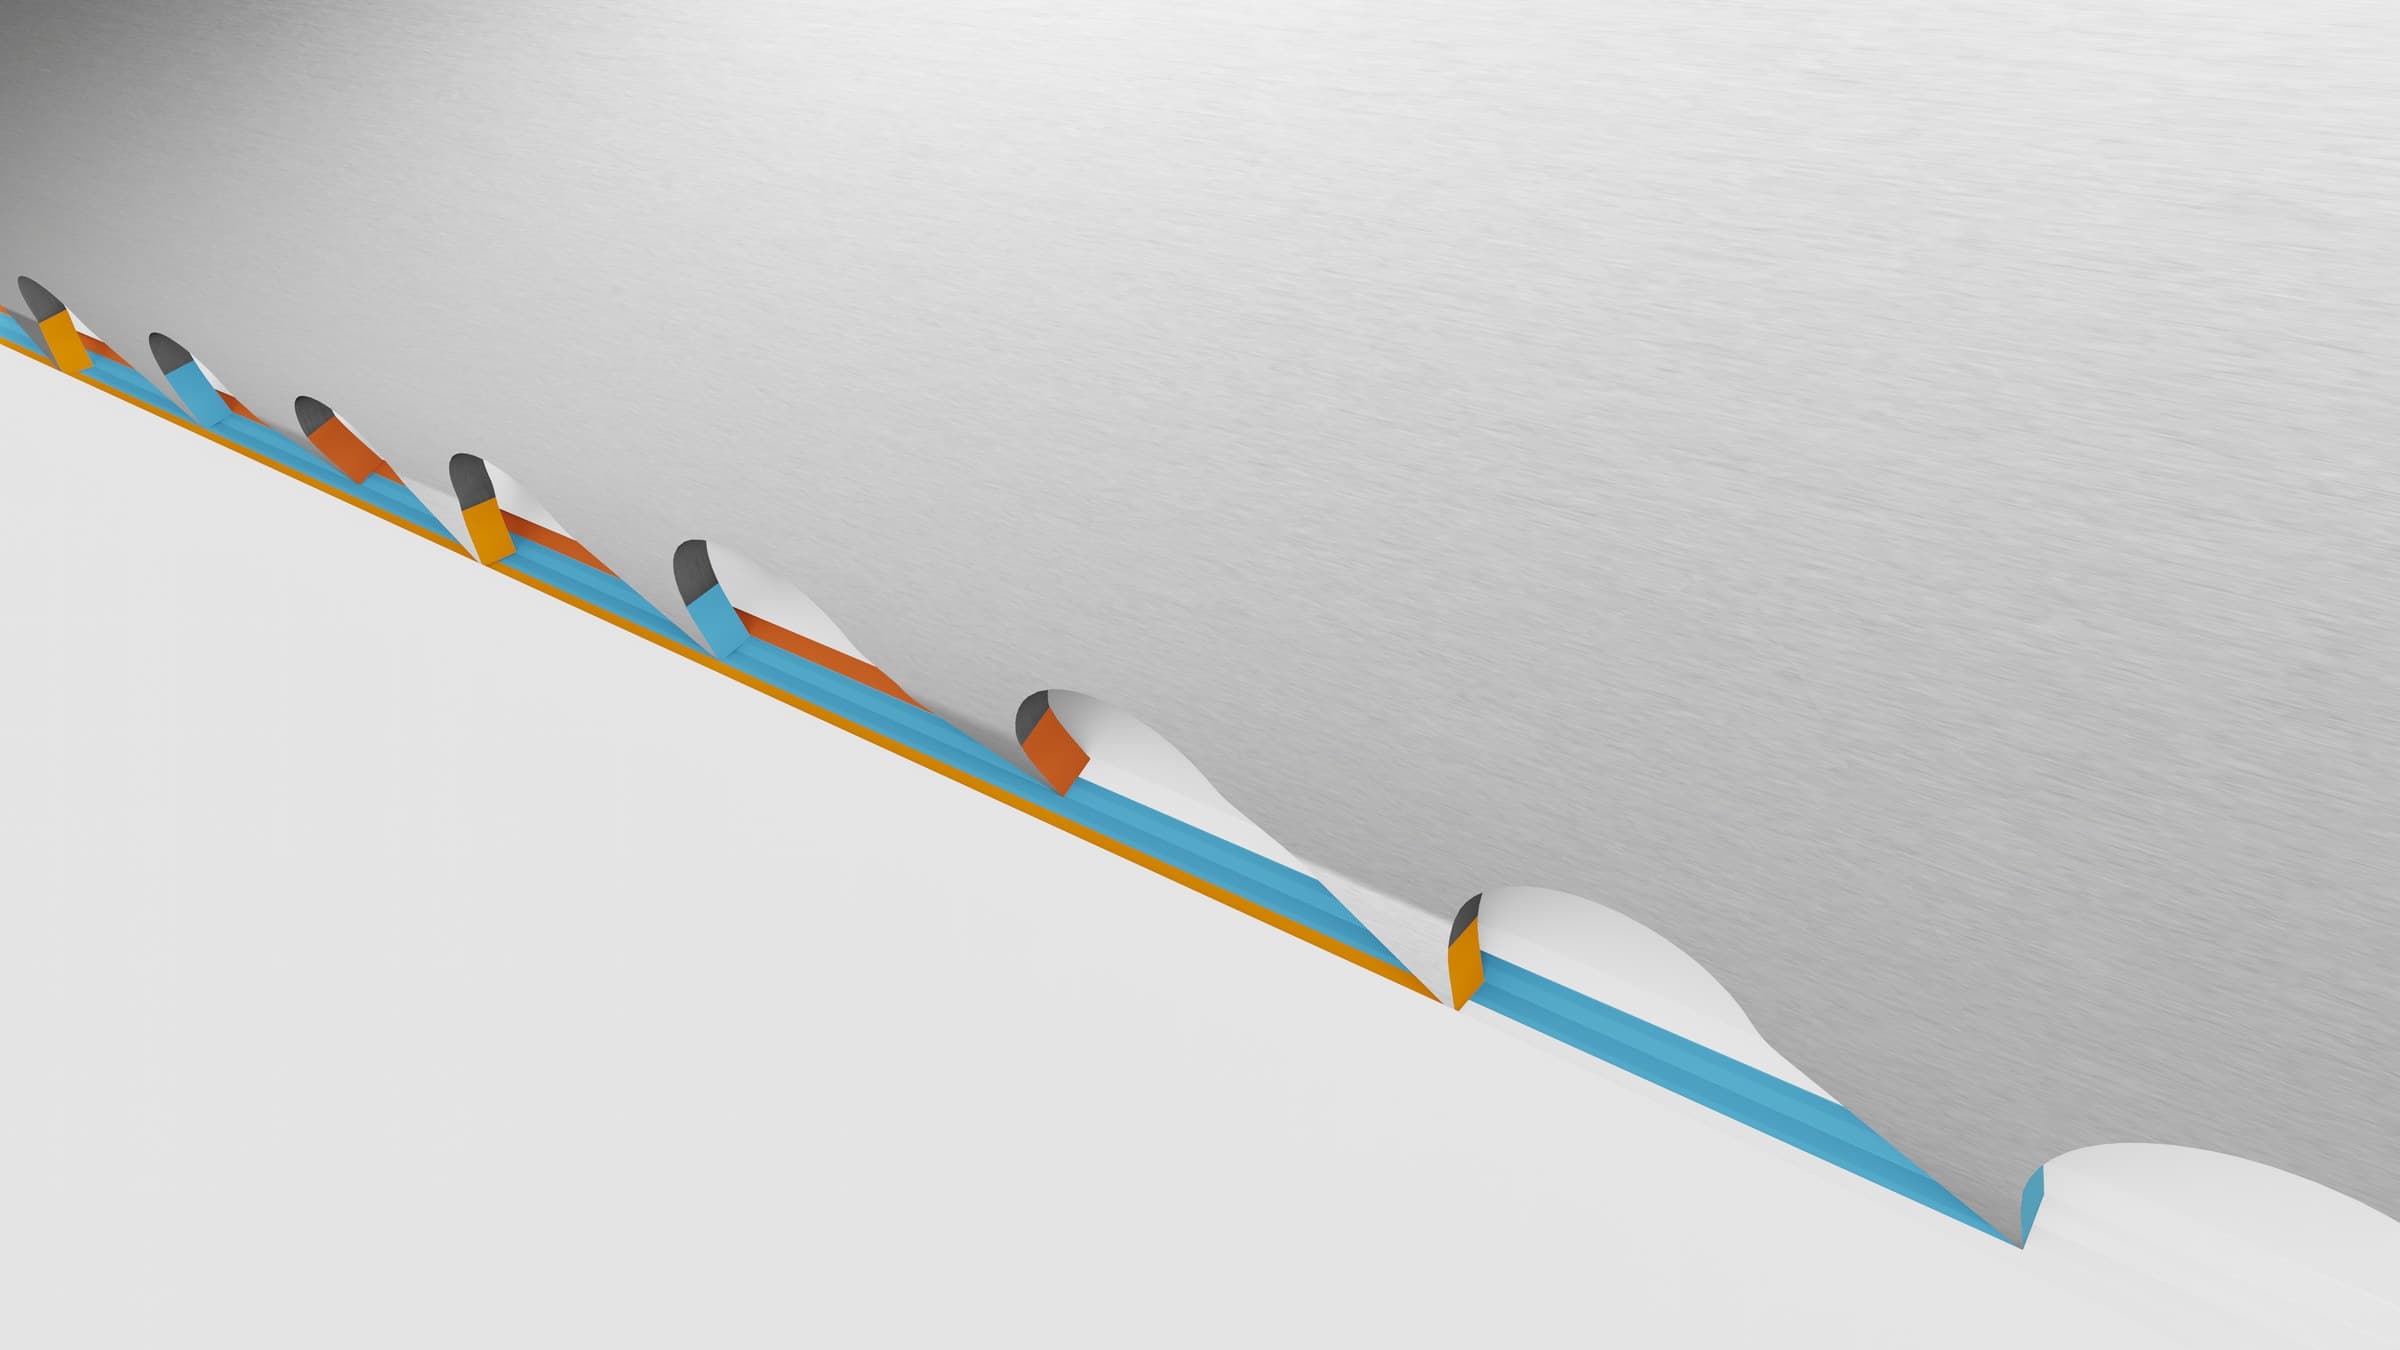
The set is the sideways angle given to the teeth. It makes the cut wider than the band body, so the body and the tooth edges clear the cut instead of rubbing. A wider set suits work where the cut tends to close on the blade. We do not publish a kerf or set width figure for this blade: ask us if your job depends on one.
All sizes
Every width, thickness, pitch and tooth form listed for this blade. Choose one to load it into the configurator.
Scroll sideways to see every pitch.
| Width x thickness | 0.7/1 TPI | 1/1.4 TPI | 1.4/2 TPI | 2/3 TPI | 3/4 TPI | 4/6 TPI | 5/8 TPI | 6/10 TPI | 8/12 TPI | 10/14 TPI |
|---|---|---|---|---|---|---|---|---|---|---|
| 27 x 0.9mm | ||||||||||
| 34 x 1.1mm | ||||||||||
| 41 x 1.3mm | ||||||||||
| 54 x 1.3mm | ||||||||||
| 54 x 1.6mm | ||||||||||
| 67 x 1.6mm |
About this blade
Bahco Sandflex Cobra 3851 is a production metal cutting bi-metal bandsaw blade built for high performance. Bahco gives it an improved HSS tooth edge over the general purpose 3851. It suits production sawing of steel including stainless, where consistent output matters more than blade price. Supplied cut to length and welded for your machine.
Specifications come from the manufacturer's published information. If the job is unusual, talk to us before you order.
Cuts these materials
Industries that use this kind of blade
Reading the TPI
TPI is the number of teeth per inch along the band. A single figure, such as 14, is a constant pitch: the teeth are evenly spaced. Two figures, such as 2/3, are a variable pitch: the spacing changes along the band between 2 and 3 teeth per inch, which breaks up vibration and lets one blade cover a wider spread of section sizes.
Read the pitch against the thickness of metal the teeth pass through. The published rule is to keep between 6 and 24 teeth in the cut: too few and each tooth takes too big a bite, too many and the gullets clog. Thick sections need a coarse pitch, thin sections and tube walls a fine one.
For tube, profiles and bundles the pitch depends on the wall thickness too. The blade finder works it out from your section and names the chart it used.
Pitch for solid sections
The published chart for solid bar, by section thickness. The rows for pitches this blade is listed in are marked.
| Section thickness | TPI |
|---|---|
| 0 to 5mm | 18 |
| 4 to 8mm | 14 |
| 2 to 15mm | 10/14 (listed for this blade) |
| 8 to 20mm | 8/12 (listed for this blade) |
| 16 to 30mm | 6/10 (listed for this blade) |
| 25 to 40mm | 5/8 (listed for this blade) |
| 35 to 70mm | 4/6 (listed for this blade) |
| 60 to 120mm | 3/4 (listed for this blade) |
| 80 to 200mm | 2/3 (listed for this blade) |
| 120 to 400mm | 1.5/2 |
| 250mm and up | 1.1/1.6 |
| 400mm and up | 0.75/1.25 |
Source: Addler (Excision) bandsaw blade tooth selection guide, corroborated by the Dakin-Flathers TPI chart. Accessed 2026-07-28. Starting recommendations from published manufacturer guidance, not guarantees. Tune at the machine.
How it compares in bi-metal blades
The nearest products in this range, compared on what the manufacturers publish. The from price is the lowest listed price for each product.
| Consideration | This product | Challenger Bandsaw Blade | Maverick Bandsaw Blade | Production M42 Bandsaw Blade |
|---|---|---|---|---|
| Range code | 3851 | Not listed | Not listed | Not listed |
| Construction | HSS tooth edge welded to a flexible alloy steel backing | HSS tooth edge welded to a flexible alloy steel backing | HSS tooth edge welded to a flexible alloy steel backing | HSS tooth edge welded to a flexible alloy steel backing |
| Cuts | Steel, Stainless steel | Structural steel, Tube, Channel | Tool steel, Stainless steel, Structural steel, Aluminium, Cast iron, Nickel alloys, Titanium alloys | Alloy steel, Stainless steel |
| Edge and tooth notes | Improved HSS tooth edge | Not listed | Not listed | Not listed |
| Widths | 27mm to 67mm | 27mm to 54mm | 27mm to 54mm | 13mm to 27mm |
| Price | From £13.12 ex VAT, £15.74 inc VAT | From £13.21 ex VAT, £15.85 inc VAT | From £13.17 ex VAT, £15.80 inc VAT | From £8.43 ex VAT, £10.12 inc VAT |
From the blog
 Carbide-tipped blades
Bi-metal vs carbide bandsaw blades, an honest decision guide
How bi-metal and carbide-tipped bandsaw blades are made, where each construction wins and how to judge them on cost per cut rather than price per blade.
 Bi-metal blades
Breaking in a new bandsaw blade, why and how
A razor-fresh bandsaw blade micro-chips under full feed. A short break-in at reduced feed hones the edge instead and repays itself in blade life.
 Bi-metal blades
M42 vs M51 bandsaw blades, when the upgrade pays
M42 and M51 are the two cobalt HSS grades on bi-metal bandsaw blades. What separates them, when M42 is enough and when M51 repays its higher price.
Frequently asked questions
What does M42 mean on a bandsaw blade?
When should I step up from M42 to M51?
How do I measure the blade length my machine needs?
Can I order a length outside the range shown?
Full measuring instructions are in our guide, How to measure a bandsaw blade length, and on the custom lengths page.
Need a different blade or a different length? Price any blade we list at the exact loop length your machine takes.
Price a custom length